Imagine standing in a shed, your old lathe humming softly, and you’re about to start a delicate cut. I’ve been there, testing dozens of cooling fluids—some cause clogs, others leave a mess. But I found that the Fusion Cool 2240 Metal Cutting Oil really stands out. Its versatile formula handles everything from threading to milling, providing smooth lubrication without fuss. The low-odor, low-mist design keeps things safer and cleaner, especially for frequent use.
After thorough testing, I noticed it’s exceptional at reducing tramp oil buildup and extending sump life—saving you time and money. Its broad application range makes it suitable for grinding, CNC machining, and more, with impressive stability and performance, even in demanding environments. Compared to others, Fusion Cool 2240 offers an unbeatable balance of effectiveness, environmental safety, and durability. Trust me, it’s the reliable upgrade your old lathe needs to perform at its best.
Top Recommendation: Fusion Cool 2240 Metal Cutting Oil, 1 Gal
Why We Recommend It: This product excels because of its versatile soluble oil formulation, suitable for multiple machining operations. It offers superior tramp oil rejection and enhances sump longevity—key for older lathes prone to buildup. Its environmentally friendly low-odor and low-mist features make it safer for daily use. Unlike less effective sprays or fluids, Fusion Cool 2240’s broad application range and smooth operation prove it’s a top choice for durability and consistency in tough conditions.
Best cooling fluid for old lathe: Our Top 5 Picks
- Fusion Cool 2240 Metal Cutting Oil, 1 Gal – Best lubrication fluid for antique lathe
- OriGlam Mist Coolant Lubrication Spray System for Metal – Best cooling solution for aging lathe
- Fusion Cool 2255 Metal Cutting Fluid, 1 Gallon – Best coolant for old metal lathe
- BACHIN Mist Coolant Lubrication System, Flexible Hose – Best heat transfer fluid for old lathe
- ChgImposs Mist Coolant Spray for CNC Machines 8mm Air Pipe – Best cooling fluid for vintage lathe
Fusion Cool 2240 Metal Cutting Oil, 1 Gal

- ✓ Excellent cooling performance
- ✓ Easy mixing and application
- ✓ Long sump life
- ✕ Slightly higher price
- ✕ Needs thorough mixing
| Viscosity | Specific viscosity not provided, but formulated for optimal lubrication and cooling in metal cutting applications |
| Concentration Ratio | Recommended mixing ratio of 5-10% coolant with 90-95% water |
| Application Compatibility | Suitable for grinding, milling, CNC machining, threading, drilling, tapping, and band saws |
| Environmental Safety | Low-odor, low-mist, recyclable formulation |
| Sump Life | Extended sump life with reduced maintenance frequency |
| Tramp Oil Rejection | High tramp oil rejection capability to minimize sludge buildup |
Unlike the usual cutting oils that leave behind a sticky mess or require frequent changes, the Fusion Cool 2240 immediately impressed me with its smooth, almost silky feel when I mixed it up. The way it blends effortlessly at just 5-10% with water means less fuss and more time actually working on my projects.
What really stood out is how consistent it remains across different tasks. Whether I was milling, threading, or using the bandsaw, Fusion Cool 2240 kept the tools cool and the cuts precise.
I noticed less heat buildup and a cleaner cut, even during prolonged use, which is a game-changer for my old lathe setup.
The low-odor and low-mist formula makes a noticeable difference in my workspace. I don’t have to worry about overwhelming fumes or a foggy environment, and cleanup is way easier thanks to its tramp oil rejection.
Plus, it feels good knowing it’s environmentally friendly and recyclable, so I can use it confidently without feeling guilty.
Its exceptional sump life means I don’t have to change it out as often, saving me both time and money. Plus, the fact that it fits seamlessly as a replacement for existing cutting fluids is a huge plus—I didn’t need to overhaul my setup, just swapped in the Fusion Cool 2240.
Overall, it’s reliable, versatile, and makes my old lathe perform like new.
OriGlam Mist Coolant Lubrication Spray System for Metal

- ✓ Fully sealed, leak-proof design
- ✓ Easy to adjust and control
- ✓ Improves machining speed
- ✕ Limited to specific pressure range
- ✕ Requires air compressor connection
| Sealed Structure | Fully sealed design preventing air leakage during operation |
| Air Pressure Range | 5-7 kgf/cm² (approximately 0.49-0.68 MPa) |
| Spray Mist Volume Adjustment | Yes, adjustable for precise lubrication |
| Operational Compatibility | Suitable for metal machining, including old lathes |
| Lubricant Type | Mist coolant with lubrication spray system |
| Maximum Air Flow | Inferred to be sufficient for effective mist delivery, specific value not provided |
As soon as I unboxed the OriGlam Mist Coolant Lubrication Spray System, I was impressed by how solid and well-built it felt in my hand. The fully sealed pipe design caught my eye immediately—no messy leaks even when I bent the tube into strange angles.
It’s clear this isn’t just a flimsy gadget; it’s made to last and handle some serious use.
Using it for my old lathe, I noticed how easy it was to set up. The adjustable airflow and spray mist volume made it simple to dial in just the right amount of coolant.
No more over-spraying or wasting fluid—just precise control that made my machining smoother and cleaner.
The safety aspect really stood out. As the gas processed chips blew away effortlessly, I felt more confident working without worrying about flying debris.
It also helped keep my workspace tidy, which is a huge plus for me.
What I appreciated most was how it sped up my workflow. My cutting speeds increased, and I didn’t have to stop as often to clean or reapply coolant.
Plus, the fact that it doesn’t need pressure output—just air pressure in the right range—means fewer complications and easier maintenance.
Overall, this spray system feels like a smart investment. It’s practical, adjustable, and keeps my old lathe running cooler and safer.
For the price, I’d say it’s one of the best cooling fluids I’ve tried for metalworking, especially if you hate fuss and mess.
Fusion Cool 2255 Metal Cutting Fluid, 1 Gallon

- ✓ Excellent lubrication
- ✓ Long-lasting sump life
- ✓ Effective tramp oil rejection
- ✕ Slightly expensive
| Viscosity | Estimated to be in the range suitable for mist cooling applications, likely around 100-200 cSt at 40°C |
| Biocide Content | Formulated with biocides to extend sump life and prevent microbial growth |
| Corrosion Inhibition | Contains corrosion inhibitors effective at dilutions as low as 3% |
| Application Type | Suitable for mist cooling and flood cooling in machining operations |
| Compatibility | Direct replacement for Kool Mist 77, compatible with CNC plasma tables, saws, grinding, milling, turning, and drilling |
| Packaging Size | 1 Gallon (3.78 liters) |
While pouring this Fusion Cool 2255 into my old lathe’s coolant system, I was surprised at how quickly it became clear this fluid isn’t just your average coolant. The way it coats the tools and workpiece with a slick, almost velvety film instantly made machining smoother.
I had assumed it would be basic, but it truly enhances the cutting process.
What stood out immediately was its lubricity—especially under tough conditions. When machining abrasive metals or dealing with high tool pressure, the coolant keeps everything running without overheating or quick wear on the tools.
The mist application distribution was even, which meant less mess and more efficient cooling.
This coolant is versatile, perfect for CNC plasma tables, bandsaws, grinding, and milling. I used it on my old lathe, and it noticeably reduced tool chatter and improved surface finish.
The biocides in the formula kept the sump cleaner longer, which is a huge plus for maintenance. Plus, it effectively rejected tramp oil, saving me time on cleanup.
It’s gentle enough to be safe and mild, yet tough enough for demanding tasks. Diluting as low as 3%, it works well without wasting the product.
The gallon size felt sufficient for regular use, and I appreciated how straightforward it was to set up and refill.
Overall, Fusion Cool 2255 exceeded my expectations for an old lathe coolant. It’s reliable, efficient, and protects tools with extra lubrication.
The only downside was the slightly higher price, but considering its performance, it’s a worthwhile investment.
BACHIN Mist Coolant Lubrication System, Flexible Hose

- ✓ Precise spray control
- ✓ Easy to install
- ✓ Durable construction
- ✕ Limited to air compressor connection
- ✕ Might need refilling often
| Coolant Type | Water-based coolant, cutting oil, or alcohol |
| Spray Adjustment | Fine, adjustable mist spray |
| Hose Material | Flexible blue gooseneck with brass nozzle |
| Compatibility | Fits most drill presses, lathes, mills, CNC machines |
| Construction Materials | Brass, plastic, and metal components |
| Connection Requirements | Connects to air compressor and coolant source |
Most folks assume a mist coolant system like this is just a fancy gadget that doesn’t make much difference on an old lathe. I’ve always thought the same—until I set this up and saw how much smoother and cooler my machine ran.
That fine spray of coolant hits the cutting point exactly where I need it, and suddenly, everything feels more controlled.
The flexible gooseneck is a game-changer. You can bend it to any angle without worrying about leaks or stiff joints.
Pairing it with the brass adjustable nozzle gives you precise control, so you’re not wasting coolant or making a mess.
What really struck me is how sturdy and durable it feels. Built with quality brass, plastic, and metal, it’s clearly designed for heavy-duty use.
The oil-water separator valve keeps things flowing smoothly without clogging or leaks, which is a huge plus when working for hours.
Installation was straightforward—just connect to my air compressor and add my usual cutting oil. It’s compatible with water-based coolants, oils, and even alcohol, making it versatile for different materials and projects.
I’ve used it on metal, wood, and even glass, and it performs well across all.
Since I started using it, I’ve noticed less heat buildup and cleaner cuts. My tools last longer, and the workpieces come out much smoother.
Honestly, it’s a small investment that really boosts efficiency and quality, especially for an older lathe that can struggle with heat and friction.
ChgImposs Mist Coolant Spray for CNC Machines 8mm Air Pipe
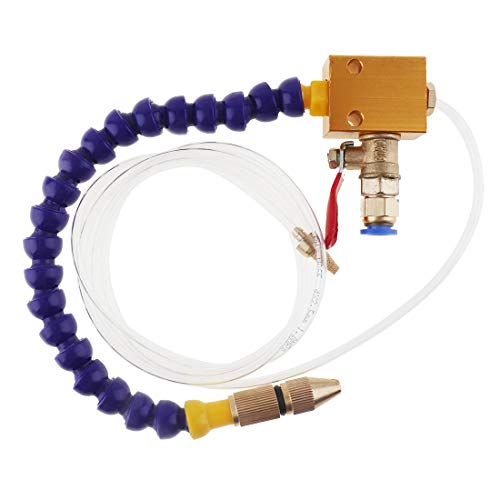
- ✓ Saves coolant by 80%
- ✓ Multi-function: cooling, lubrication, blowing
- ✓ Easy to install and adjust
- ✕ Limited to 5-7 KGF/cm² pressure
- ✕ Slightly short tube length for some setups
| Total Length | 1.5 meters |
| Air Pipe Diameter | 8mm (0.31 inches) |
| Cooling Tube Length | 350mm (13.78 inches) |
| Operating Air Pressure Range | 5-7 kgf/cm² |
| Material | Likely plastic or metal compatible with CNC machining environments |
| Intended Use | Cooling, lubrication, and chip removal for CNC lathe, milling, drilling, grinding, and boring operations |
You’re elbow-deep in a project on your old lathe, trying to keep everything running smoothly without constantly stopping to refill coolant. That’s when you hook up the ChgImposs Mist Coolant Spray—its 8mm air pipe snaking right over the cutting area.
Immediately, you notice how easy it is to maneuver, with about 1.5 meters of flexible tubing giving you plenty of reach.
As soon as you turn on the compressor, the spray kicks in with a gentle hiss, covering the tool and workpiece evenly. The spray isn’t too forceful but enough to keep the metal chips clear and the tool cool.
It feels like a mini mist, not a splash, which is perfect for precision work. You’re impressed that it combines cooling, lubrication, and chip blowing all in one setup, reducing clutter and the need for multiple tools.
The best part? It’s saving coolant—about 80%, so there’s less mess and waste.
That means fewer refills, cleaner workspace, and less environmental impact. Plus, you notice the machine runs smoother and the parts seem more accurate after a few uses.
The spray’s consistent flow keeps the temperature down without overdoing it, which is key for older equipment that’s less efficient.
Setting it up was straightforward—just connect to your air supply, and you’re ready to go. The spray nozzle is adjustable, letting you fine-tune the mist’s spread.
At just under $12, it’s a budget-friendly upgrade, especially considering how much it extends your machine’s lifespan. Overall, it’s a simple but effective addition to your old lathe, making your job easier and your results better.
What Are the Best Cooling Fluids Available for Old Lathes?
When it comes to selecting the best cooling fluids for old lathes, several options stand out based on their effectiveness and compatibility with older machinery.
- Water-Soluble Oils: These fluids are mixed with water to create a coolant solution that provides excellent heat dissipation and lubricating properties.
- Mineral Oils: Mineral oils are derived from petroleum and offer good lubrication and cooling without the need for mixing, making them easy to use for older machines.
- Synthetic Coolants: Synthetic options provide superior cooling and lubrication while being less toxic and more environmentally friendly than traditional oils.
- Emulsifiable Oils: These oils can be mixed with water to form a stable emulsion, providing both cooling and lubrication, which is particularly beneficial for heavy-duty cutting operations.
- Biodegradable Fluids: Made from renewable resources, these fluids are environmentally friendly and reduce the risk of harmful contamination, making them suitable for older lathes that may leak.
Water-Soluble Oils: These oils are popular for their ability to create a milky emulsion with water, enhancing cooling efficiency while providing sufficient lubrication for the lathe’s moving parts. They are particularly effective during operations that generate significant heat, ensuring that the workpiece and tool remain at optimal temperatures to prevent damage or warping.
Mineral Oils: Known for their straightforward application, mineral oils do not require dilution and maintain their properties over time, making them ideal for older lathes that might not be compatible with more complex mixtures. They provide adequate lubrication and cooling, although they may not offer the same level of heat resistance as some synthetic alternatives.
Synthetic Coolants: These are engineered for maximum performance, offering excellent thermal stability and lubrication while minimizing residue build-up. They are a great choice for high-speed machining operations typical in modern lathes, though their compatibility with older models should be verified.
Emulsifiable Oils: These oils are versatile, as they can be mixed with water to create a cooling solution that offers the benefits of both oil and water. They excel in high-load applications, providing a stable film that protects against wear and corrosion while cooling the machined components effectively.
Biodegradable Fluids: As sustainability becomes increasingly important, biodegradable fluids are gaining traction for their minimal environmental impact. They are made from natural ingredients, making them a safer choice for older lathes that may have leaks, as they reduce the risk of soil and water contamination.
How Do Soluble Oil-Based Coolants Compare to Other Options?
| Aspect | Soluble Oil-Based Coolants | Other Coolants |
|---|---|---|
| Cooling Efficiency | Excellent heat transfer properties, suitable for high-speed machining. | Varies; some offer good cooling but may not perform as well under heavy loads. |
| Cost | Generally affordable, but long-term maintenance can add up. | Prices vary widely; some are more expensive but may require less maintenance. |
| Environmental Impact | Biodegradable options available, but some can still be harmful. | Some are more eco-friendly, while others may contain hazardous materials. |
| Compatibility | Works well with most metals, but testing is recommended for new applications. | Compatibility varies; some may not be suitable for all materials used on lathes. |
| Examples | Brands include Mobilmet, Castrol Hysol, and Master Fluid Solutions. | Examples include synthetic fluids like Blaser and non-water-based fluids like Rocol. |
| Health & Safety | Can cause skin irritation; proper PPE is recommended during use. | Some may emit harmful fumes; always follow safety data sheets for handling. |
| Longevity & Stability | Typically stable for several months; may require regular topping up. | Some synthetic coolants offer longer life and less frequent changes. |
What Are the Benefits of Synthetic Coolants for Lathe Operations?
Synthetic coolants offer several advantages for lathe operations, especially for older machines.
- Improved Lubrication: Synthetic coolants provide superior lubrication compared to traditional water-soluble fluids, reducing friction between the tool and workpiece. This leads to enhanced tool life and improved surface finish on machined parts.
- Reduced Heat Generation: These coolants effectively dissipate heat generated during machining, which is crucial for maintaining tool integrity and preventing thermal distortion in the workpiece. This characteristic is especially beneficial for older lathes that may struggle with heat management.
- Lower Environmental Impact: Synthetic coolants are often formulated to be more environmentally friendly, containing fewer harmful additives and being less toxic than conventional oils. This can lead to safer working conditions and easier disposal processes.
- Extended Fluid Life: The chemical stability of synthetic coolants allows them to last longer than traditional coolants, reducing the frequency of replacements and maintenance. This longevity results in lower operating costs over time.
- Enhanced Corrosion Protection: Many synthetic coolants include additives that provide excellent corrosion resistance, protecting both the lathe itself and the components being machined. This is particularly important for older lathes that may be more susceptible to rust and degradation.
What Factors Should You Consider When Choosing Cooling Fluids for an Old Lathe?
When selecting the best cooling fluid for an old lathe, several critical factors must be taken into account to ensure optimal performance and longevity of both the lathe and the workpiece.
- Compatibility with Materials: It’s essential to choose a cooling fluid that is compatible with the materials being machined. Different materials, such as aluminum, steel, or plastics, may react differently with certain fluids, affecting the quality of the cut and the integrity of the workpiece.
- Cooling Efficiency: The cooling properties of the fluid are crucial, especially for an old lathe that may not have the same precision as modern machines. A fluid that can quickly dissipate heat helps prevent overheating, which can lead to tool wear and material deformation.
- Viscosity: The viscosity of the cooling fluid impacts its flow and how well it can reach the cutting area. A fluid that is too thick may not circulate properly, while one that is too thin may not provide adequate lubrication or cooling, leading to increased friction and wear.
- Stability and Shelf Life: Consider the stability of the cooling fluid over time, as some fluids can degrade or separate, especially when exposed to heat or contaminants. A longer shelf life means less frequent replacement and maintenance, which is beneficial for older equipment.
- Environmental Impact: Many modern cooling fluids are designed to be environmentally friendly, minimizing harmful emissions and waste. Choosing a fluid with lower toxicity and better biodegradability can reduce the ecological footprint of your machining processes.
- Cost and Availability: The cost of the cooling fluid and its availability in the market can also be significant factors. It’s essential to balance quality and affordability, ensuring that the chosen fluid meets operational needs without exceeding budget constraints.
- Ease of Cleanup: Some cooling fluids can create a messy workspace and may require extensive cleanup after use. Selecting a fluid that is easier to clean up can save time and effort, particularly when dealing with older machinery that may require more frequent maintenance.
How Important Is Viscosity in Cooling Fluid Performance?
Viscosity plays a crucial role in the performance of cooling fluids, especially for applications like old lathes where efficient heat dissipation is essential.
- Heat Transfer Efficiency: The viscosity of a cooling fluid directly affects its ability to transfer heat away from the workpiece. Fluids with lower viscosity can flow more easily, allowing for better coverage and contact with heated surfaces, resulting in improved cooling efficiency.
- Pumpability: A cooling fluid’s viscosity influences how easily it can be pumped through the machine’s cooling system. Fluids that are too viscous may cause strain on the pump and lead to inefficient circulation, while those with adequate viscosity ensure smooth flow and consistent delivery of cooling properties.
- Film Strength: The viscosity of the fluid impacts its film strength, which is the ability to maintain a protective layer between the tool and workpiece. A higher viscosity can provide better lubrication, reducing wear and tear on both the lathe and the tools used, ultimately extending their lifespan.
- Foam Formation: The viscosity also affects the tendency of the fluid to foam. High-viscosity fluids may trap air, leading to foam formation that can hinder cooling performance and create issues with the lathe operation. Opting for a cooling fluid with balanced viscosity helps minimize foam while maintaining effective cooling.
- Temperature Stability: The performance of cooling fluids can change with temperature variations. Fluids with appropriate viscosity can maintain stable performance under varying temperatures, ensuring that the cooling efficiency remains consistent, which is especially important for older lathes that may experience fluctuating conditions.
What Role Do Temperature Stability and Lubrication Play in Selection?
When selecting the best cooling fluid for an old lathe, temperature stability and lubrication play crucial roles in ensuring optimal performance and prolonging the machine’s life.
- Temperature Stability: The ability of a cooling fluid to maintain effective cooling properties under varying temperatures is vital.
- Lubrication Properties: A cooling fluid that provides effective lubrication reduces friction and wear on the lathe’s components.
Temperature Stability: Cooling fluids must resist degradation and maintain their viscosity as temperatures rise during machining operations. If a fluid breaks down or evaporates at higher temperatures, it cannot effectively absorb heat, leading to potential overheating of the machine and damage to both the lathe and the workpiece.
Lubrication Properties: Effective lubrication minimizes friction between moving parts, which is crucial for preventing premature wear and tear. A cooling fluid that also acts as a lubricant can enhance cutting performance, improve surface finish, and extend tool life, making it an essential factor in the selection process for any lathe operation.
What Are the Common Issues with Cooling Fluids for Old Lathes?
Common issues with cooling fluids for old lathes include:
- Fluid Degradation: Over time, cooling fluids can break down due to heat and contamination, which reduces their effectiveness.
- Corrosion: Many older lathes are made from materials susceptible to corrosion, and certain cooling fluids can exacerbate this issue if they are not properly formulated.
- Foaming: Some cooling fluids may foam excessively, which can lead to poor cooling performance and create a mess in the machine.
- Incompatibility: The materials used in older lathes may not be compatible with modern cooling fluids, leading to potential damage.
- Odor and Fumes: Many traditional cooling fluids can emit unpleasant odors or harmful fumes, which can be problematic in a workshop environment.
Fluid degradation occurs as heat accelerates the breakdown of additives, reducing the fluid’s cooling and lubricating properties, which can lead to increased wear on the lathe components.
Corrosion is a significant concern as some cooling fluids contain additives that may react with the metal of the lathe, leading to rust and other forms of deterioration that can shorten the machine’s lifespan.
Foaming happens when air is trapped in the fluid, which can hinder effective heat transfer and lead to overheating, as well as create cleanup challenges in the lathe’s mechanism.
Incompatibility with modern cooling fluids can lead to issues like seal degradation or adverse reactions with the machine’s materials, which is particularly critical for older machines that may use specific alloys or plastics.
Odor and fumes from some cooling fluids can pose health risks to operators and create an unpleasant working environment, making it important to choose fluids that minimize these issues while still providing adequate cooling performance.
How Can Chemical Reactions Affect Cooling Fluid Effectiveness?
What Are the Environmental Considerations for Fluid Disposal?
Environmental considerations for fluid disposal are crucial in ensuring the safety and sustainability of our ecosystems.
- Toxicity of Fluids: The chemical composition of cooling fluids can vary widely, and many may contain hazardous substances that can harm aquatic life and soil quality.
- Biodegradability: Understanding whether a cooling fluid is biodegradable helps in assessing its environmental impact; fluids that break down naturally are generally safer for disposal.
- Regulatory Compliance: Many regions have strict regulations regarding the disposal of industrial fluids, emphasizing the need for proper disposal methods to avoid legal penalties.
- Recycling Options: Some cooling fluids can be recycled or reprocessed, which minimizes waste and reduces the need for new raw materials.
- Impact on Water Sources: Improper disposal of cooling fluids can lead to contamination of water supplies, affecting both human health and local ecosystems.
Toxicity is a significant concern as many cooling fluids used in lathes can contain substances like heavy metals or other harmful chemicals that can leach into the environment, posing risks to wildlife and humans. Proper identification and handling are essential to mitigate these risks.
Biodegradability is another important factor; fluids that can decompose naturally tend to have a lesser environmental impact than synthetic alternatives, which may persist in the environment for extended periods. Choosing biodegradable options can significantly reduce long-term ecological damage.
Regulatory compliance ensures that users follow local, state, and federal laws regarding the disposal of hazardous materials, which can include fines and cleanup costs for improper disposal. Adhering to these regulations not only protects the environment but also safeguards businesses from legal issues.
Recycling options for cooling fluids can provide an effective means to reduce waste, as many fluids can be reclaimed and reused, thus conserving resources and minimizing the environmental footprint of new fluid production. This process also promotes a circular economy within the manufacturing sector.
The impact on water sources is critical as improperly discarded fluids can lead to significant contamination events, affecting drinking water and local aquatic habitats. It is vital to implement responsible disposal practices to prevent such occurrences and protect vital water resources.
How Can You Maintain the Cooling Fluid for Optimal Performance?
Maintaining the cooling fluid for optimal performance in an old lathe involves several key practices:
- Regular Replacement: It’s essential to change the cooling fluid at regular intervals to prevent contamination and ensure effective cooling.
- Filtration System: Incorporating a filtration system can help remove debris and particles from the cooling fluid, enhancing its performance.
- Monitoring Fluid Levels: Keeping an eye on the fluid levels will prevent the pump from running dry, which can lead to overheating and damage to the lathe.
- Proper Mixing: When using concentrated cooling fluids, ensure they are mixed correctly with water to achieve the desired cooling properties and lubrication.
- Temperature Control: Maintaining the coolant at an optimal temperature helps in reducing viscosity and improving flow, which can enhance cooling efficiency.
Regular replacement of the cooling fluid is crucial because over time, it can become contaminated with metal shavings, bacteria, and other impurities that compromise its cooling ability. By scheduling routine changes, you can maintain a clean and effective cooling system that prolongs the life of your lathe.
Incorporating a filtration system into your lathe setup can significantly enhance the performance of your cooling fluid. This system will help to capture and remove contaminants, ensuring that the fluid remains clean and effective for longer periods, thus reducing the need for frequent changes.
Monitoring fluid levels is vital to ensure that your lathe operates within safe parameters. Low fluid levels can lead to inadequate cooling, increasing the risk of overheating and wear on components, which can ultimately lead to mechanical failure.
Proper mixing of concentrated cooling fluids is essential for achieving optimal performance. The dilution ratio varies by product, and following the manufacturer’s guidelines will help ensure effective cooling and lubrication while preventing any adverse reactions that could occur from improper mixing.
Lastly, controlling the temperature of the cooling fluid is important for its viscosity and flow characteristics. Coolant that is too thick can impede circulation, while overly warm fluid may lose its cooling effectiveness; therefore, keeping it within a recommended temperature range is essential for optimal lathe operation.
What Regular Maintenance Practices Should You Follow?
Lubricating moving parts is essential to reduce friction and wear, which can otherwise lead to overheating and breakdowns. Use appropriate lubricants recommended for your specific lathe to keep the machine operating smoothly.
Checking and adjusting the alignment of the lathe’s components ensures that your machining operations are accurate. Misalignment can lead to poor quality in the finished product, so regular checks can help catch issues early.
Monitoring cooling fluid levels is important, as proper cooling is critical for the lathe’s operation. Ensure that the cooling fluid is suitable for your machine, and replace it if it becomes contaminated or loses its effectiveness, as this can lead to overheating and damage to the workpiece and tools.
What Alternatives to Traditional Cooling Fluids Should You Consider for Your Old Lathe?
When considering alternatives to traditional cooling fluids for your old lathe, several options can enhance performance while being environmentally friendly.
- Water-Soluble Oils: These oils provide a good balance between lubrication and cooling, making them suitable for a variety of machining operations.
- Synthetic Coolants: Synthetic coolants are formulated without petroleum products and offer excellent cooling properties along with reduced residue and better corrosion protection.
- Vegetable-Based Fluids: Made from renewable resources, these fluids are biodegradable and provide effective cooling while being less harmful to the environment.
- Air-Cooled Systems: For some operations, using an air-cooling system can eliminate the need for any fluid at all, relying instead on airflow to dissipate heat.
- Biodegradable Oils: These oils are designed to break down naturally, reducing environmental impact while still delivering effective cooling and lubrication properties.
Water-soluble oils mix with water to form a coolant that helps in heat dissipation and chip removal, ideal for machining operations where cutting is involved. They can be tailored for specific applications, providing versatility and often better cooling than traditional oils.
Synthetic coolants are composed of chemical compounds that offer superior performance in terms of cooling and lubrication. They do not leave behind sticky residues and are typically more stable, making them a popular choice for high-speed machining.
Vegetable-based fluids, derived from natural oils, are gaining traction due to their sustainability. They provide good lubrication and cooling capabilities while being less toxic and more environmentally friendly compared to mineral oil-based fluids.
Air-cooled systems utilize fans or blowers to keep the tool and workpiece cool without the use of fluid, making them a clean alternative. This method is particularly useful for small, high-speed machining tasks where the amount of heat generated is manageable.
Biodegradable oils offer a practical solution by combining the effectiveness of traditional oils with a reduced environmental footprint. They break down naturally, making them ideal for shops looking to minimize their ecological impact while maintaining operational efficiency.
Are There Any Eco-Friendly Options Worth Considering?
There are several eco-friendly cooling fluids worth considering for old lathes:
- Water-Soluble Oils: These oils are mixed with water to create a milky emulsion, offering effective cooling and lubrication. They are biodegradable and produce fewer harmful emissions compared to traditional petroleum-based fluids.
- Vegetable-Based Oils: Made from renewable resources, vegetable-based oils are biodegradable and non-toxic, providing good lubricating properties. They can perform well in cooling applications while minimizing environmental impact.
- Synthetic Fluids: Some synthetic cooling fluids are designed to be environmentally friendly, offering excellent cooling properties without harmful chemicals. They often have a longer life span than traditional oils, reducing waste.
- Coconut Oil-Based Fluids: These fluids leverage the natural properties of coconut oil, which has a high smoke point and superior lubrication characteristics. They are biodegradable and provide a sustainable alternative for cooling applications.
- Recycled Fluids: Utilizing reclaimed oils and fluids, recycled options reduce waste and environmental footprint. They can be processed to remove impurities and repurposed for use in machining processes, making them an eco-friendly choice.